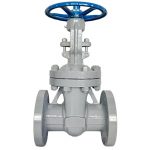
I. Important Attribute and Specification Description
A. Global Standard Compliance & Product Core Definition
B. Quantified Complete Technical Performance Parameters
| Parameter Category | Standardized Verified Performance Index |
|---|---|
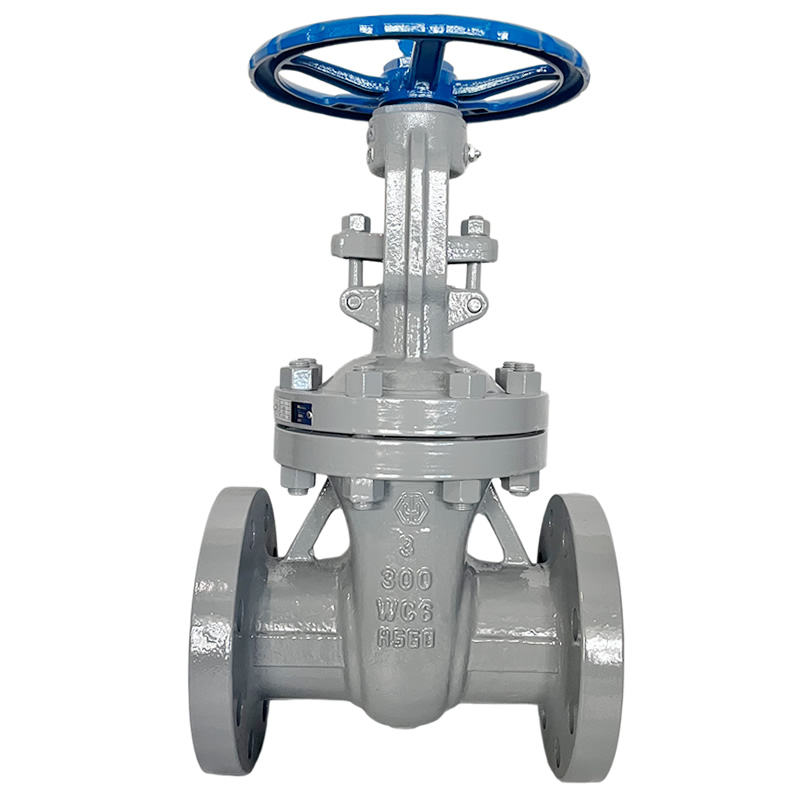
| Nominal Pipe Size | 3 Inch (DN80) |
| Pressure Class Rating | Class 300LB following ASME B16.34 industrial pressure grade standard |
| Main Valve Body Material | ASTM A217 WC6 Chromium Molybdenum Alloy Cast Steel |
| Stem Sealing Packing Material | Flexible Graphite Braided Composite Packing |
| End Connection Form | RF Raised Face Flanged Connection matching ASME B16.5 bolt hole layout |
| Operation Mode | Manual Cast Iron Blue Handwheel with Rising Stem Visual Position Indicator |
| Stem Base Material | ASTM A182 F12 Cr-Mo Alloy Steel |
| Gate Disc Trim Material | Solid SS316 Austenitic Stainless Steel with Precision Lapped Sealing Surface |
| Applicable Continuous Working Temperature Range | -29°C ~ +570°C, applicable to high-temperature steam, thermal oil, hydrocarbon gas and neutral industrial liquid media |
| Shell Hydrostatic Test Benchmark | 1.5 times of Class 300LB rated nominal working pressure regulated by API 598 |
| Seat Tightness Testing Criterion | 1.1 times of rated working pressure with ANSI B16.104 Class VI zero bubble leakage performance |
| Standard Face-to-Face Dimension | Fixed dimensional specification regulated by ASME B16.10 rising stem gate valve standard |
| Flow Passage Characteristic | Full bore straight flow channel with extremely low flow resistance when fully opened |


II. Manufacturing Technology and Core Product Features
A. Full Process Standardized Manufacturing & Multi-Stage Strict Quality Control Mechanism
- Raw Material Inbound Inspection Management: All incoming WC6 alloy casting ingots, F12 alloy stem bar stock, solid SS316 disc blanks and flexible graphite packing raw materials are delivered to factory physical and chemical inspection laboratory for spectral composition analysis and mechanical property sampling test. Only raw material batches that pass chemical component ratio calibration, tensile strength, hardness and high-temperature creep performance verification can be released to subsequent processing flow; unqualified raw material batches are directly returned to upstream suppliers to block defective source inflow into production links.
- Precision Casting and Stress Relief Heat Treatment: Valve body and bolted bonnet blanks adopt high-precision sand casting technology to shape straight-through full-bore internal flow channel, effectively reducing casting defects including sand holes, shrinkage cavities and cold shut. After casting forming, blanks are placed in segmented temperature control furnace for normalization and tempering compound heat treatment to homogenize internal metal grain structure and eliminate casting residual internal stress, improving overall structural high-temperature impact resistance of valve body. Post heat treatment finished blanks implement 100% MT magnetic particle inspection and UT ultrasonic non-destructive flaw detection complying with ASME V specification, eliminating invisible internal and surface crack defects that threaten long-term high-temperature pipeline service safety.
- High Precision CNC Machining of Critical Sealing Components: Valve body seat sealing circular surface, bonnet stem through hole, stem outer circle and flanged positioning surface are processed by five-axis linkage CNC machining center with strict micron-level dimensional tolerance control. The matching sealing surfaces of seat and SS316 gate disc undergo fine turning and manual grinding lapping treatment to reach Ra 0.8μm or lower surface roughness value, ensuring complete close fitting between sealing pairs after assembly to achieve zero leakage shut-off effect. The F12 alloy stem outer circular surface adopts centerless precision grinding to obtain mirror smooth outer diameter, reducing friction abrasion loss between stem and flexible graphite packing during continuous lifting and rotating movement.
- Flexible Graphite Packing Forming and Pre-Compression Treatment: Braided flexible graphite packing strips are cut and formed according to standard dimensional parameters, each packing ring set receives fixed tonnage hydraulic pre-compression to eliminate elastic shrinkage deformation risk under later high-temperature working pressure fluctuation. Random sampled packing pieces from each production lot carry out high-temperature accelerated aging simulation test inside constant temperature thermal chamber to verify long-term dynamic sealing stability under periodic drastic temperature cycling environment.
- Dust-Free Assembly and Complete Finished Product Performance Test: Full valve assembly operation is finished inside independent dust-free assembly workshop; all bonnet fastening bolts are locked by calibrated digital torque wrench following unified standardized torque value to avoid uneven gasket compression causing static sealing failure at body-bonnet joint. After assembly completion, all finished valves sequentially experience shell hydrostatic pressure test, seat air tightness leakage test, full-stroke open-close cycle endurance test and high-temperature thermal stability inspection formulated by API 598 specification. Products failing any single testing item enter designated rework flow instead of being stored in finished product warehouse; only fully inspected qualified units go through surface anti-corrosion epoxy coating and standard export wooden box packaging before shipment to global end users and international EPC contractors.
B. Distinctive Core Structural Product Features
- Full Straight Through Full Bore Flow Channel Design: The internal double disc gate structure without any protruding barrier inside the pipeline realizes unobstructed straight medium circulation when fully opened, minimizing fluid pressure loss and pipeline transmission energy consumption, the core structural advantage of gate valves compared with globe and butterfly valves with curved flow passages.
- Ultra-High Temperature Resistant WC6 Cr-Mo Alloy Steel Valve Body: Selected ASTM A217 WC6 chromium molybdenum alloy steel raw material has outstanding high-temperature oxidation resistance and anti-creep performance, stably adapting to long-term continuous high-temperature pipeline working conditions that ordinary carbon steel valves cannot bear, covering steam and thermal oil medium service up to 570°C.
- Corrosion Resistant Solid SS316 Stainless Steel Gate Disc Trim: Integrated SS316 gate disc provides excellent resistance to chloride ion and weak acid medium erosion, avoiding rust and pitting corrosion damage of carbon steel trim under complex industrial fluid environment, precision lapped metal sealing surface maintains Class VI zero leakage shut-off performance for long service cycles.
- Multi-Layer Flexible Graphite Stem Dynamic Sealing System: Braided flexible graphite packing set breaks through the temperature limit of ordinary PTFE plastic packing, maintaining stable stem fugitive emission control performance under continuous ultra-high temperature working conditions without melting, aging or permanent plastic deformation, fully conforming to global VOC environmental emission control regulatory requirements.
- Heat Treated Anti-Galling F12 Cr-Mo Alloy Steel Valve Stem: Quenched and tempered F12 alloy steel stem matches the high-temperature performance of WC6 valve body, balances surface hardness and core material toughness, resisting medium corrosive erosion and reciprocating friction galling during long-term full stroke operation, effectively avoiding gate disc stuck failure caused by stem rust and abrasion loss.
- Standard ASME B16.5 RF Flanged End Connection Layout: Raised face flanged structure fully complies with international ASME dimensional standards, seamlessly matching all mainstream global standard industrial pipeline flanges, serrated flange surface enhances gasket anti-slip performance and long-term pipeline static sealing stability under pressure surge impact.
- Labor-Saving Manual Blue Cast Iron Handwheel Rising Stem Operation Unit: Solid blue painted cast iron handwheel with enlarged operation radius reduces manual rotation torque required for full valve stroke switching even under maximum Class 300LB differential pressure; external rising stem structure provides real-time visual valve opening position indication without auxiliary monitoring equipment installation for convenient on-site field operation management.
- Full-Set International Authoritative Certification Endorsement: Entire product research, production and finished testing workflow passes ISO9001 quality management system audit, EU CE safety certification and API 598 performance verification, all dimensional and performance indicators meet North American and European mainstream industrial procurement standards to smoothly access international EPC global tendering project procurement lists.
III. Comprehensive Multi-Dimensional Product Competitive Advantages
- Ultra-Low Flow Resistance Reduces Long-Term Pipeline Operation Energy Consumption: Full straight-through full bore flow channel eliminates medium turbulence and flow blocking structure, cutting pipeline fluid pressure loss by more than 50% compared with globe valves, continuously lowering power consumption of supporting pumps and compressors for end-user factories and reducing daily production operation expenditure year by year.
- Extraordinary High-Temperature Service Adaptability Unique to Cr-Mo Alloy Material: WC6 alloy steel body can stably operate under ultra-high temperature steam and thermal oil working conditions that WCB carbon steel valves cannot withstand, expanding the applicable temperature range of pipeline isolation equipment, becoming irreplaceable matching parts for boiler main steam pipeline and thermal power high-temperature auxiliary piping systems.
- Extended Service Lifecycle Cuts Long-Term Plant Spare Part Procurement Expense: Benefiting from corrosion-resistant solid SS316 gate disc, anti-galling F12 alloy stem and wear-resistant metal hard sealing pair, the valve maintains stable zero-leakage isolation performance over thirteen years under standard rated working conditions, effectively reducing end-user factory spare valve purchasing expenditure and pipeline shutdown production loss triggered by frequent valve replacement and maintenance work.
- Ultra-Wide Medium and Temperature Adaptation Coverage Scope: Matching combination of WC6 high-temperature alloy body, F12 anti-corrosion alloy stem, flexible graphite high-temperature packing and SS316 anti-corrosion metal sealing trim enables consistent stable operation in diversified media covering ultra-high-temperature superheated steam, thermal conduction oil, crude oil, natural gas, industrial circulating water and neutral solvent within temperature span from minus 29°C up to 570°C, realizing unified single valve model to satisfy multiple different production working condition matching demands for industrial manufacturing enterprises.
- Optimized Total Ownership Cost Control for End User Factories: WC6 alloy steel raw material has balanced initial procurement cost compared with high-grade duplex stainless steel valve alternatives; zero leakage metal sealing structure eliminates economic loss generated by valuable medium leakage and subsequent environmental governance fines caused by high-temperature fugitive emissions, and low-maintenance packing design reduces routine overhaul labor and material expenditure, comprehensively lowering full lifecycle operation cost of the valve for factory operators.
- Convenient On-Site Maintenance Structure Shortens Pipeline Shutdown Duration: Bolted bonnet split design allows maintenance staff to disassemble bonnet, extract internal stem and SS316 gate disc components without removing the entire valve from the pipeline, greatly shortening pipeline shutdown overhaul time and minimizing production interruption economic loss caused by routine valve maintenance work.
- Strict Global Environmental Compliance Property: Flexible graphite stem packing restricts volatile fugitive medium leakage under high-temperature working environments, fully complying with stringent EU Industrial Emission Directive and US EPA VOC emission control standards, becoming core selection advantage for thermal power and petrochemical enterprises passing regular environmental compliance audit inspection.
- Stable Anti-Water Hammer Performance for Pipeline Safety Protection: Double disc gate structure opens and closes slowly under medium pressure buffering, which effectively weakens pipeline water hammer impact generated by sudden medium backflow and pump startup/shutdown, protecting downstream pipeline equipment such as heat exchangers, pressure vessels and flow meters from impact damage and improving overall high-temperature pipeline operation safety.
IV. Global Multi-Industry Industrial Application Scopes
- Thermal Power & Cogeneration Power Plant Industry: Extensively installed on boiler main superheated steam delivery pipeline, high-temperature condensate recovery circulating loop piping and turbine auxiliary isolation pipeline of thermal power stations, WC6 alloy body bears long-term ultra-high temperature steam scouring without thermal deformation, full bore flow channel reduces steam transmission pressure loss, and zero leakage metal sealing prevents high-temperature steam backflow damage to boiler feedwater pumps and precision turbine equipment, serving as core isolation equipment for power station high-temperature piping systems.
- Petrochemical & Crude Oil Refining Plant: Deployed on high-temperature thermal oil circulation pipeline, crude oil cracking main transmission pipeline and high-temperature hydrocarbon gas isolation piping inside large-scale refinery plants, solid SS316 gate disc resists corrosion of sulfide-containing high-temperature oil and gas media, flexible graphite packing eliminates flammable medium fugitive leakage risk under high temperature, and full straight flow channel optimizes medium transmission efficiency of refining production lines.
- Central Heating & Industrial High-Temperature Steam Supply Pipeline Network: Selected for large industrial park high-temperature thermal oil heating trunk pipeline and cogeneration power plant external steam supply main pipeline, standard ASME flanged connection matches industrial heating pipeline construction standards, compact rising stem layout adapts limited space workshop and outdoor pipe rack installation environment, stable isolation performance completely cuts off medium circulation during pipeline maintenance to guarantee construction safety.
- Oil & Gas Midstream Transmission Station & Thermal Recovery Storage Tank Farm: Installed on high-temperature crude oil transmission pipeline and thermal recovery wellhead isolation piping of oil and gas transfer stations, WC6 alloy steel adapts high-temperature crude oil service environment, low flow resistance reduces long-distance oil transmission energy consumption, metal hard sealing avoids flammable crude oil leakage safety hazards under variable pressure working conditions.
- Metallurgy & Non-Ferrous Metal Smelting Factory: Adopted on high-temperature waste heat recovery steam pipeline and hot flue gas circulation isolation piping inside metallurgical smelting production line, ultra-high temperature resistant WC6 body fits harsh continuous high-temperature medium working environment of smelting workshop, full bore flow channel ensures unobstructed circulation of high-temperature waste gas and steam to maximize waste heat recovery efficiency.
- General Chemical Processing & Thermal Oil Heating Workshop: Used on high-temperature neutral solvent circulation pipeline and thermal oil heating loop piping of chemical manufacturing workshops, SS316 gate disc resists weak acid and chloride ion medium erosion, convenient disassembly bonnet design facilitates regular internal dirt cleaning for media containing tiny solid particle impurities, stable isolation performance provides safe pipeline cut-off guarantee for workshop equipment overhaul.
RELATED
-
API 609 ASME B16.5 Class150 NPS10 ASTM B148 C95800 Nickel Aluminum Bronze Manual Double Offshore Eccentric Flanged Butterfly Valve
I. Important Attribute Specifications A. Material Composition TIANYU double eccentric butterfly valve is constructed with corrosion-resistant alloy ma…
-
API 600 ASME B16.5 Class 150 NPS 1“ ASTM B148 C95800 Nickel Aluminum Bronze Flexible Wedge OS&Y Flanged Gate Valve with Handwheel Operation for Marine Seawater Offshore and Coastal Industrial Piping
I. Important Attribute Specifications A. Material Composition TIANYU flexible wedge gate valves are engineered with a material matrix carefully select…
-
API594 ASME 6“ Class150LB Replaceable Rubber Liner & SS304 Blade Ductile Iron Wafer Manual Slurry Knife Gate Valve
I. Important Attribute and Specification Description A. Global Standard Compliance & Product Core Definition The TIANYU Wafer Slurry Knife Gate Va…
-
API 602 ASME DN80 Class 300LB ASTM A216 WCB Manual Flanged Straight Pattern Globe Valve With Metal-to-Metal Trim with Flexible Graphite Stem Packing
I. Important Attribute and Specification Description A. Global Standard Compliance & Product Core Definition The TIANYU Straight Pattern Globe Val…
-
API 594 ASME B16.5 CE DN80 Class 150LB ASTM A216 WCB Flanged Swing Check Valve
I. Important Attribute and Specification Description A. Global Standard Compliance & Product Core Definition The TIANYU Swing Check Valve is a bol…
-
API 609 ASME B16.34 ASME B16.5 CE 4 Inch Class 600LB UNS S32750 4A Wafer Type Triple Eccentric Butterfly Valve
I. Important Attribute and Specification Description A. Global Standard Compliance & Product Definition Developed and fabricated under the full su…